CuW70 · 70% Tungsten
W/Cu 70/30 Electrode Wheels
Higher conductivity for heavy-current welding
Tungsten 70% ±2%, balance copper · MOQ: None for standard sizes · Lead time: 10–14 days standard · 20–25 days custom
Overview
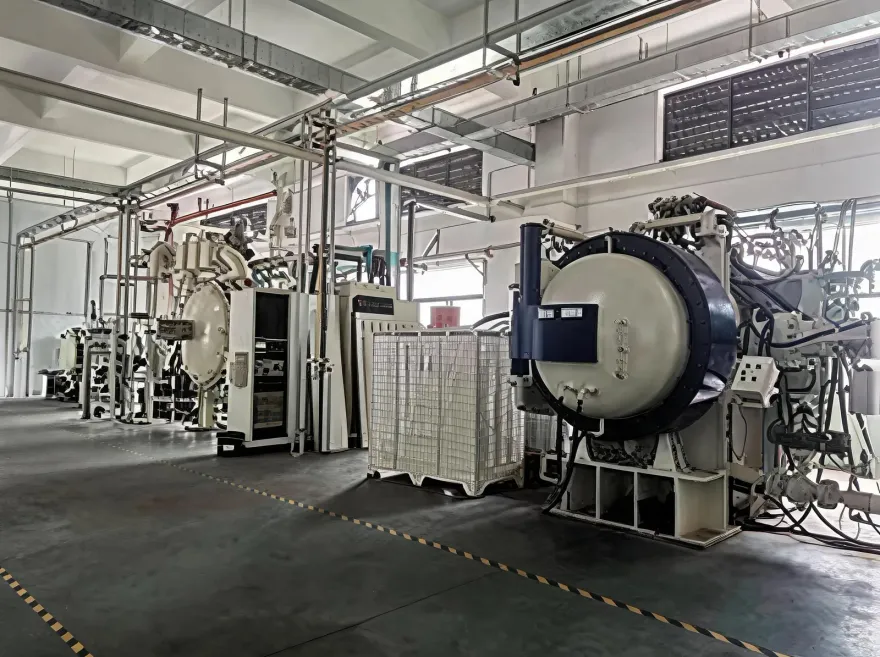
Made by infiltration, finished by machining
When your seam-welding schedule demands more current, the 70/30 grade moves heat faster: roughly 25% higher electrical conductivity than 75/25, at the cost of some erosion life. Many customers stock both grades and switch by weld schedule.
Same production route — infiltration, sintering, finish machining — and the same tolerance package: OD 0/+0.5 mm, bore H7, runout 0.02 mm. Supplied with a batch traceability record on request.
Material values shown are typical for the grade. Per-batch composition, density and hardness reports are provided on request — see quality control.
| Composition | W 70% ±2%, Cu balance (CuW70) |
| Density | ≈ 14.5 g/cm³ (typical) |
| Hardness | ≈ 175 HB (typical) |
| Electrical conductivity | ≈ 42% IACS (typical) |
| Max dimensions | OD 400 mm × thickness 100 mm |
| Tolerances | OD 0/+0.5 mm · thickness ±0.1 mm · bore H7 · runout 0.02 mm |
| Edge profiles | Flat · single/double bevel · R profile · knurled |
| Lead time | 10–14 days standard · 20–25 days custom |
| MOQ | None for standard sizes |
Typical applications
- Heavy-current seam welding
- Welding of coated and high-resistivity steels
- Projection welding fixtures
- General resistance-welding consumables
In depth
Engineering notes
Where the extra conductivity pays
Roughly 25% higher conductivity than 75/25 means less resistive heat generated in the wheel itself for the same current schedule. On thick stock, high-speed lines, or any schedule already near the ceiling of your transformer and secondary circuit, that difference shows up as a cooler wheel face, less sticking, and a wider usable current window.
The trade is erosion life: the softer composite dresses faster under the same electrode force. On lines that dress on a fixed interval anyway, the faster dress rate costs little — which is why 70/30 is the default on can-body and tube-mill lines that maintain their wheels on schedule.
Switching between grades
Both grades are produced on the same infiltration line and machined on the same cell, so switching a station from 75/25 to 70/30 — or running one station on each — is a purchasing decision, not a process change. Bore, OD, profile and tolerances are identical across grades; only the material values differ.
A practical approach many customers take: stock 75/25 for the stations where wheel life limits the campaign, 70/30 for the stations where heat limits it. Both stay in supply from stock shapes with no minimum order.
Traceability and inspection
Every batch is checked for composition, density and hardness, and a batch traceability record ships on request. For buyers running automotive or food-can lines that require incoming inspection paperwork, we can include dimensional inspection records per wheel — bore, OD, runout and thickness — against the drawing revision you hold.
Third-party stamped test reports to ASTM B702 are available when your quality system needs an external certificate rather than a factory report.
Technical library
Further reading
The guides engineers read before they write the second drawing.
- W75Cu25 vs W70Cu30 for resistance welding When the extra conductivity is worth the wear life — and which weld schedules actually need it.
- Seam welding galvanized and coated steel The zinc pickup problem, and how alloy choice changes your cleaning interval.
- Wheel wear cycles and a spare strategy How many spares to hold so a reorder never turns into a line stoppage.
- Wheel slip and uneven wear: causes and fixes Diagnose skid marks and one-sided wear before blaming the alloy.
Also from the same floor
Pair it with
 Best seller
CuW75 · 75% Tungsten
W/Cu 75/25 Electrode Wheels
The workhorse alloy for seam-welding wheels
View specs
 Stock shapes
CuW75 / CuW70
Electrode Rods & Blocks
Stock shapes machined from infiltration bar
View specs
To drawing CuW75 / CuW70
Threaded Electrodes
Precision-threaded welding consumables
View specs
Need W/Cu 70/30 on a drawing?
Send alloy, dimensions and quantity — quote back within 24 hours.